- Trapezoidal Machine
- Corrugated Machine
- Glazed Tile Machine
- Double Layer Machine
- CZU Purlin Machine
- Ridge Cap Machine
- Floor Decking Machine
- Rolling Door Machine
- Fence Machine
- Embossing Machine
- Standing Seam Machine
- Cut To Length And Slitting Line
- Guard Rail Machine
- Decoiler And Stacker
- Stud And Track Machine
- Gutter And DownPipe
- Curving Machine
- Cladding Panel Machine
- Corollary Equipment

- Trapezoidal Machine
- Corrugated Machine
- Glazed Tile Machine
- Double Layer Machine
- CZU Purlin Machine
- Ridge Cap Machine
- Floor Decking Machine
- Rolling Shutter Door Machine
- Palisade Fence Machine
- Embossing Machine
- Standing Seam Machine
- Cut To Length And Slitting Line
- Guard Rail Machine
- Decoiler And Stacker
- Stud And Track Machine
- Gutter And DownPipe
- Curving Machine
- Cladding Panel Machine
- Corollary Equipment
- Other
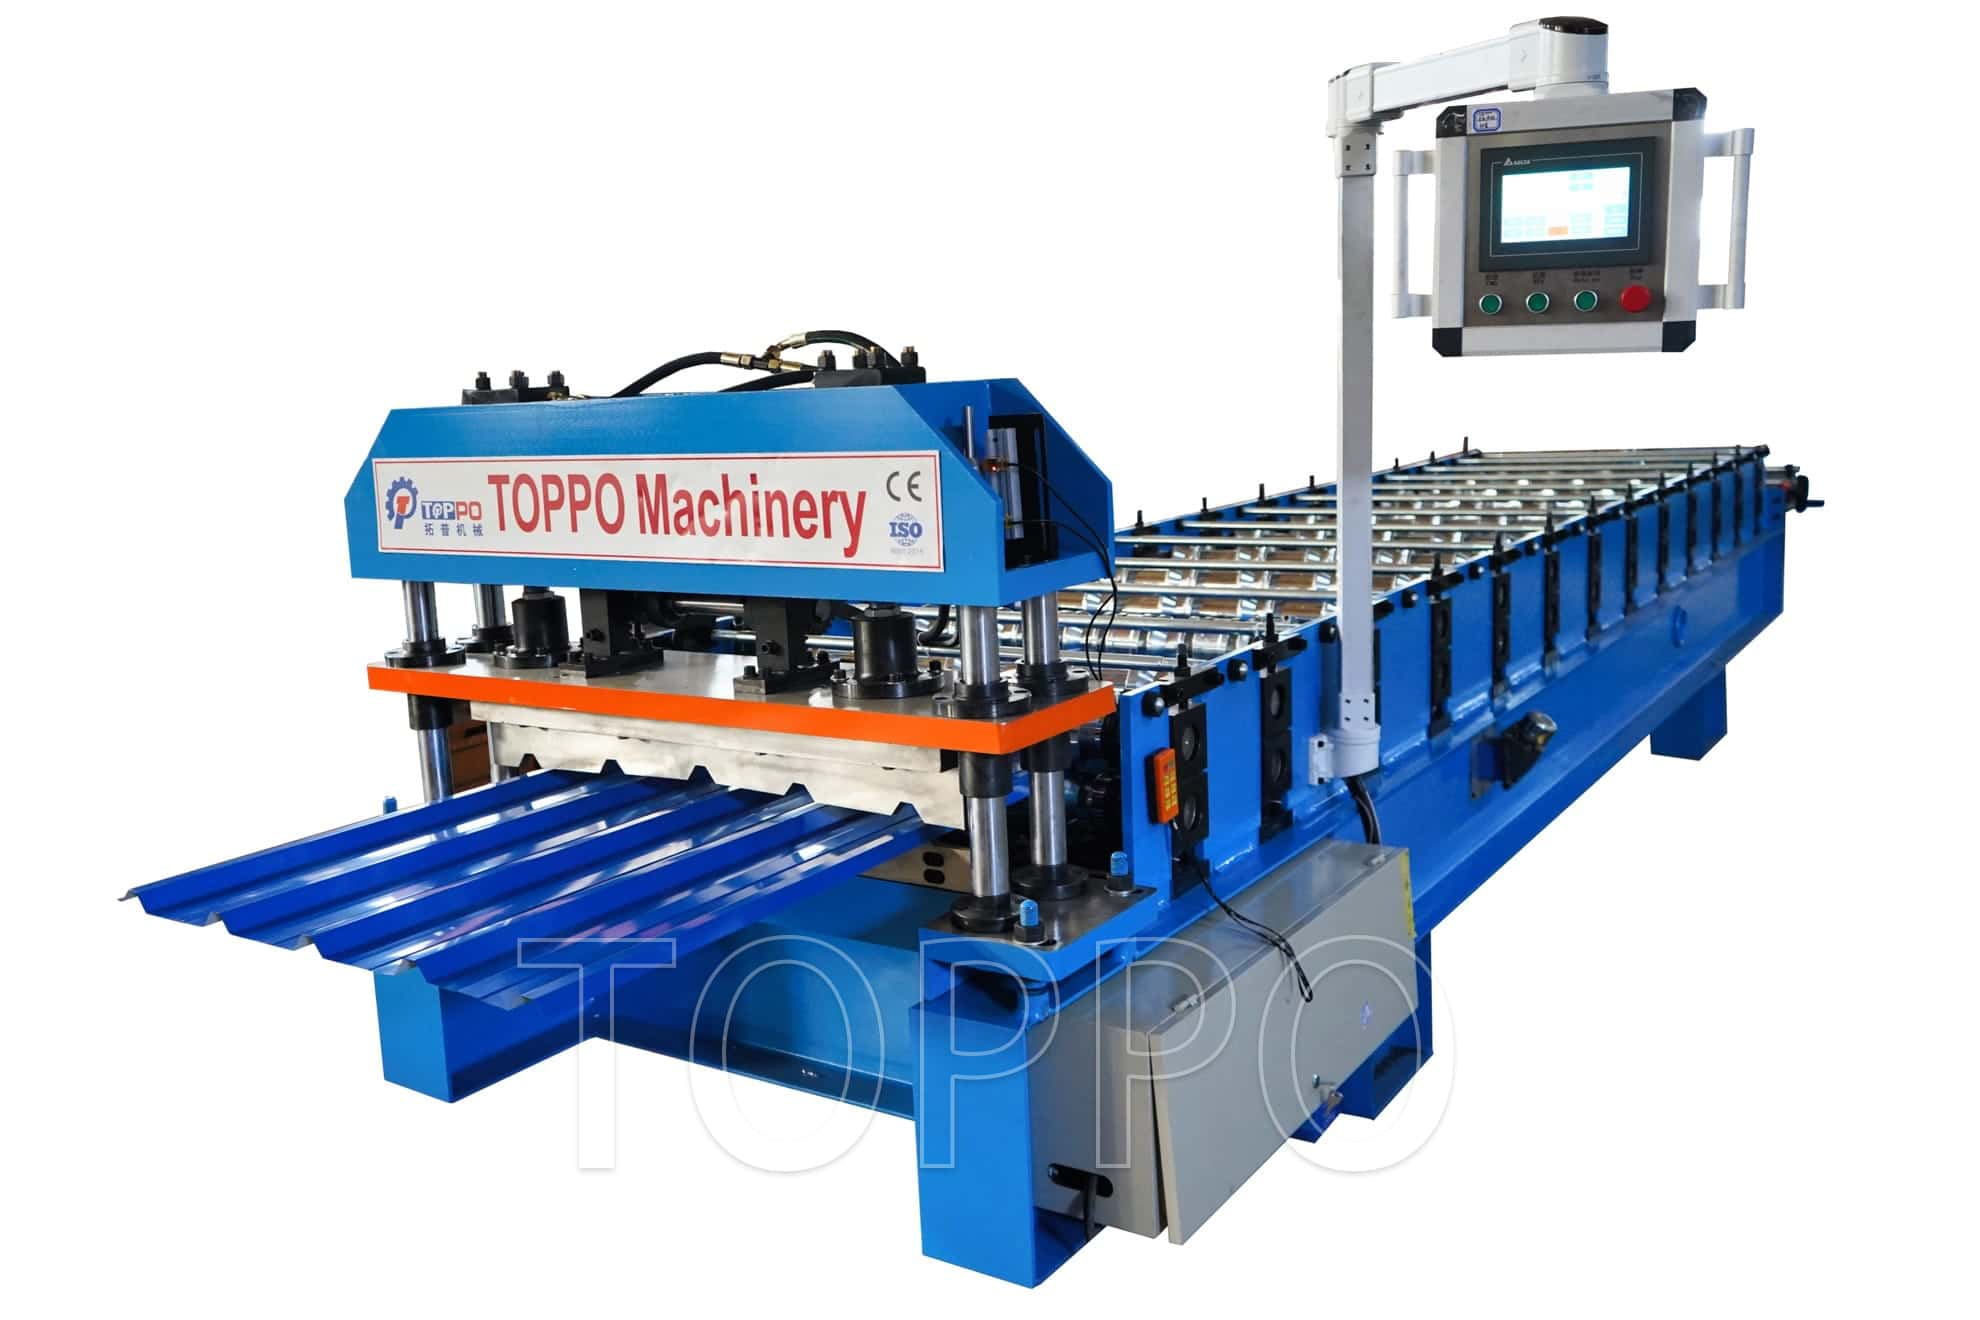
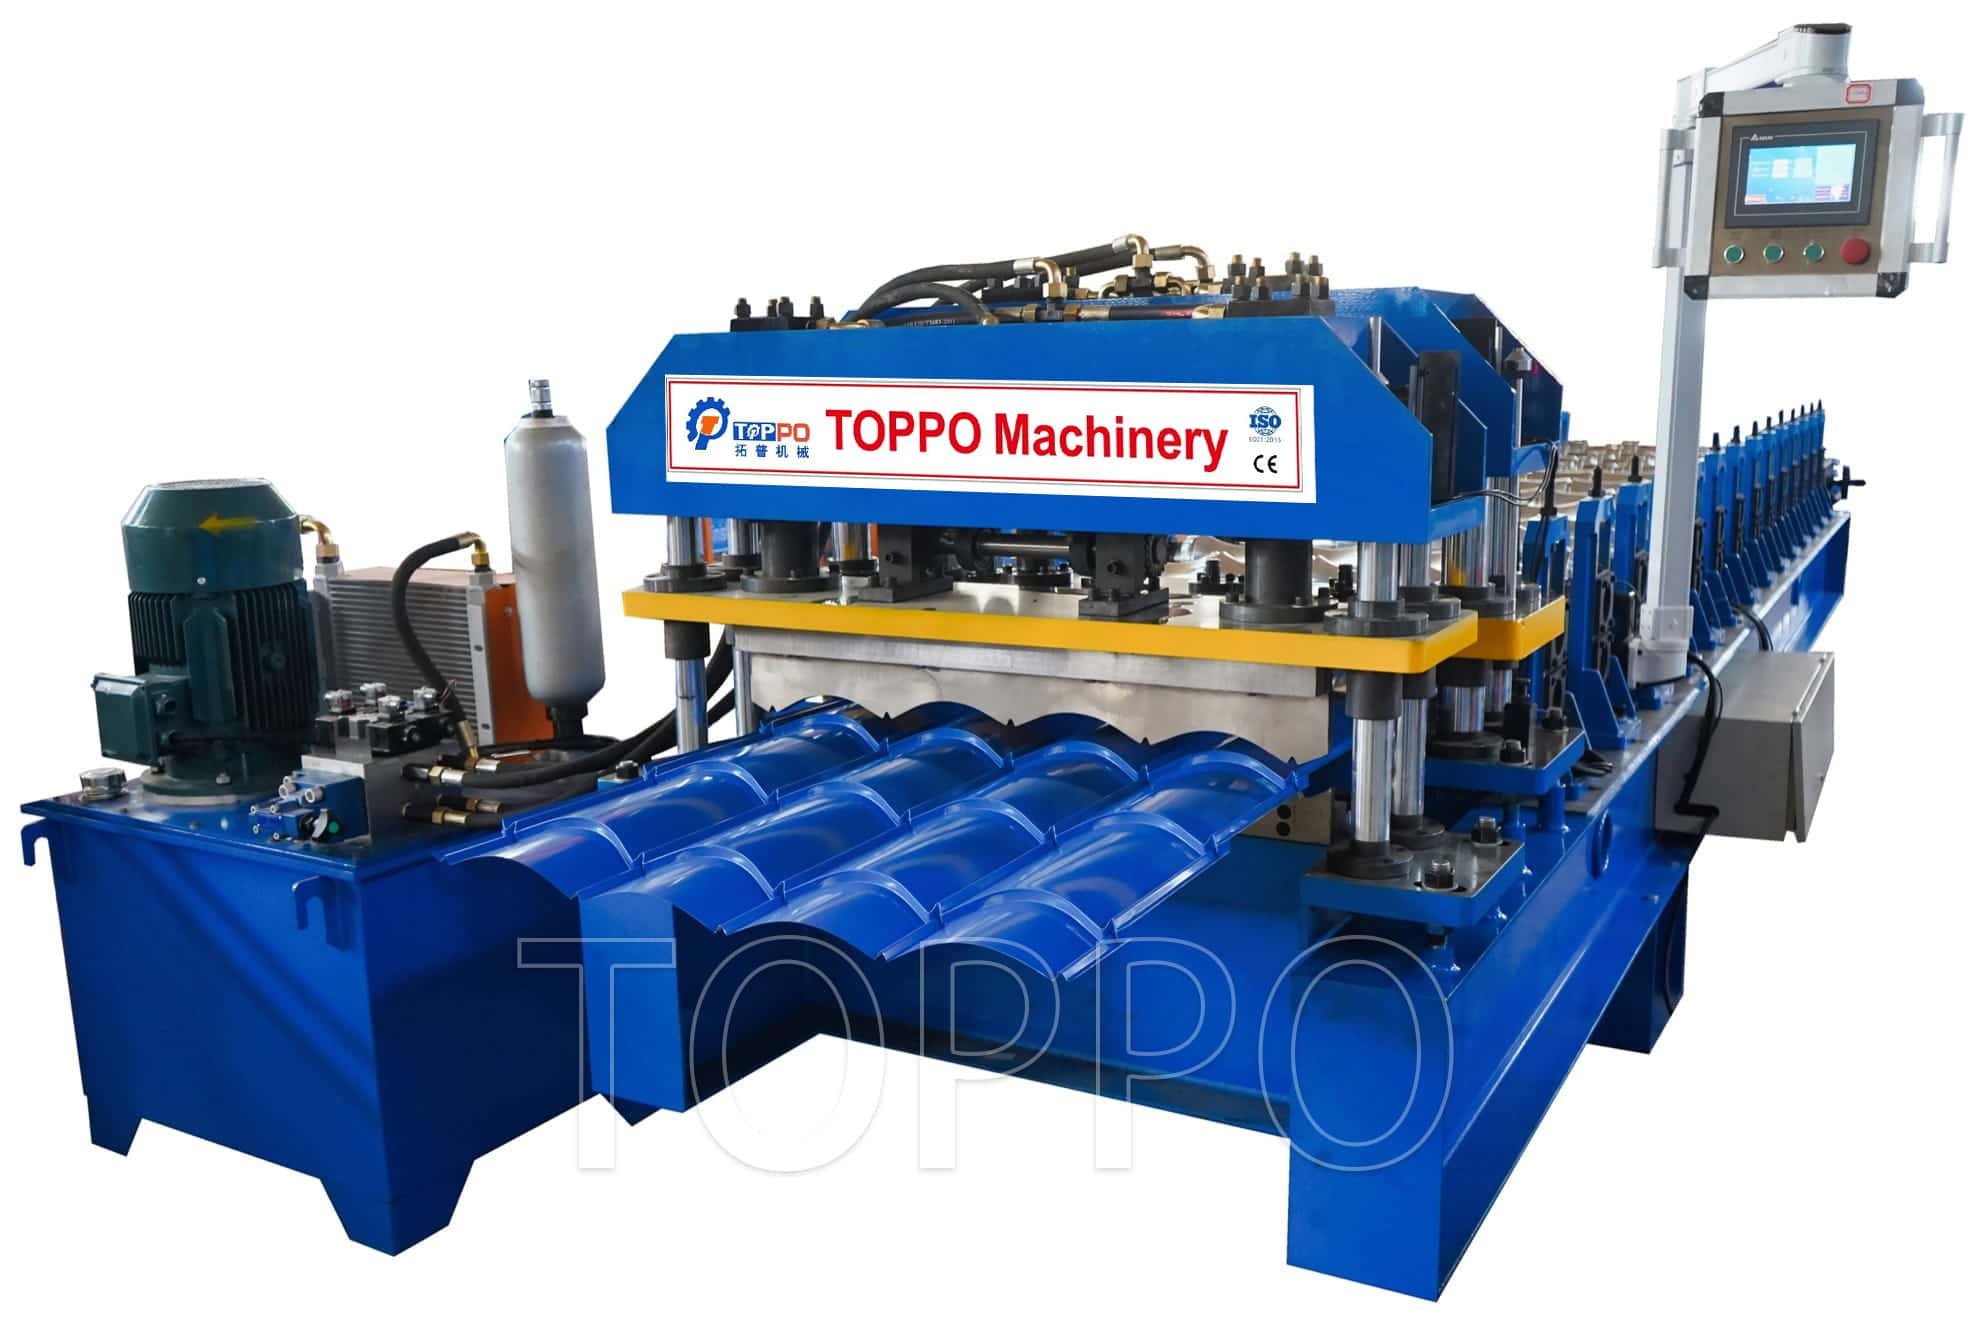
Hydraulic Glazed Tile Roofing Making Machine
This glazed tile roofing making machine is developed for producing decorative metal roof panels with a classic tile appearance and the practical advantages of modern coated steel roofing. The finished sheets are lightweight, strong, weather-resistant, easy to transport, and fast to install. They are widely used for villas, residential houses, resorts, pavilions, light-steel buildings, warehouses, factories, commercial properties, and renovation projects.
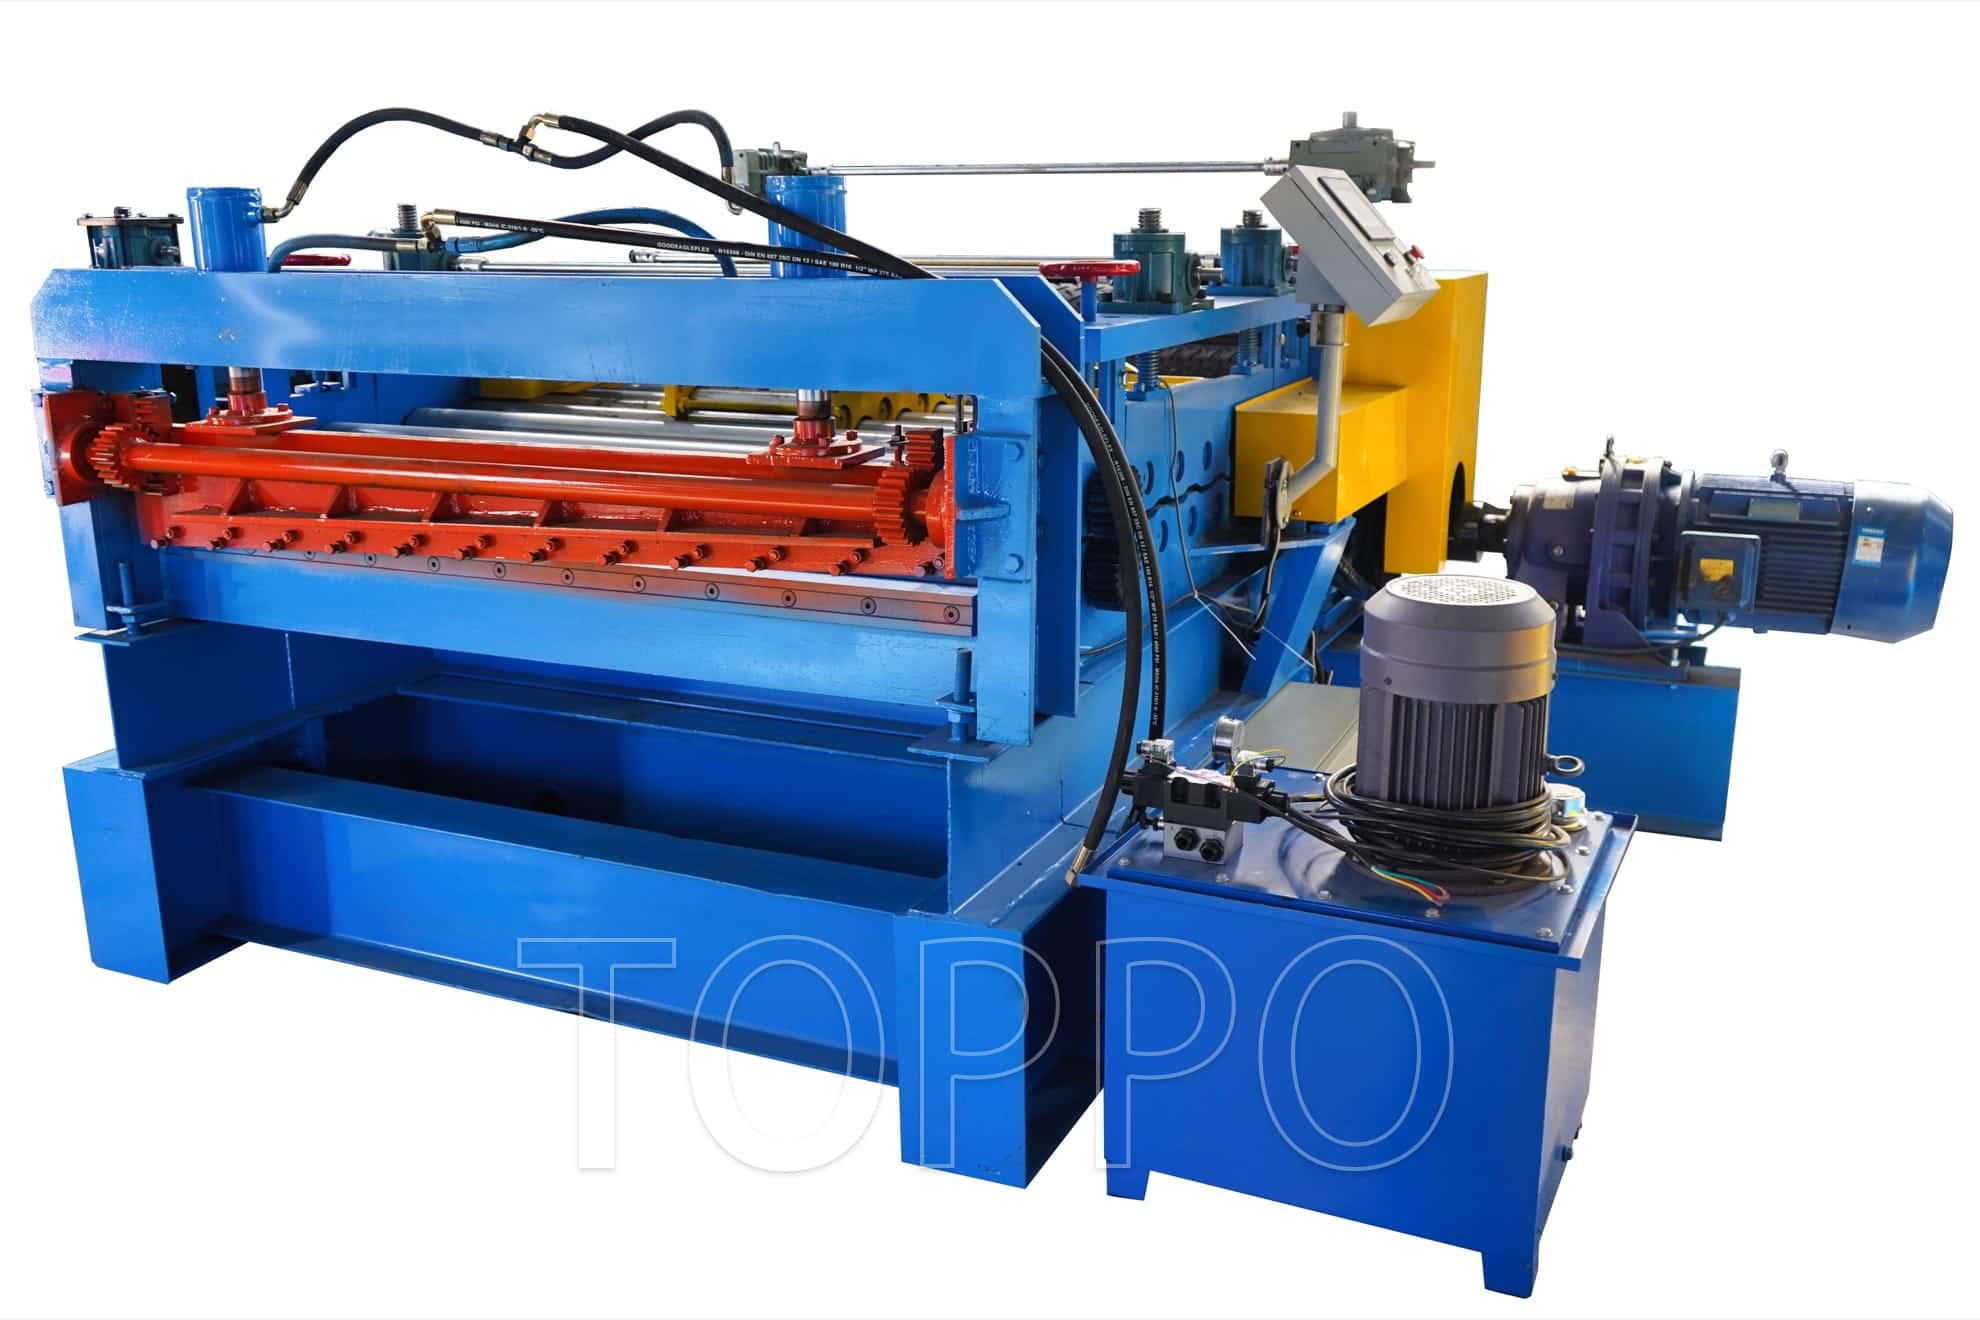
The production line shown uses a rigid welded base, multiple precision forming stations, a hydraulic step-pressing and profile-cutting section, an independent hydraulic power pack, and a movable touch-screen operator panel. The left-front layout provides convenient access to the pressing area, cutting assembly, hydraulic components, and control interface. Final machine dimensions and technical values are engineered according to the confirmed roof panel drawing and raw-material specification.
Why Choose This Machine
Combines roll forming, tile-step pressing, measuring, counting, and cutting in one coordinated line.
PLC control improves repeatability of panel length, batch quantity, and step position.
Hydraulic pressing creates a clear three-dimensional tile pattern for an attractive finished roof.
Gradual multi-pass forming helps maintain sheet shape and reduce coating damage.
Heavy-duty steel construction supports alignment, operating stability, and long service life.
Custom engineering allows the line to match regional roofing profiles and electrical standards.
Production Flow
Coil loading → material guiding → optional leveling → multi-station roll forming → hydraulic tile-step pressing → encoder measuring → hydraulic cutting → finished-sheet receiving or automatic stacking.
Product Attributes and Technical Configuration
| Attribute | Typical Specification or Description |
|---|---|
| 1. Product Name | Hydraulic Glazed Tile Roofing Making Machine |
| 2. Machine Type | Automatic metal roof tile cold roll forming line |
| 3. Main Application | Production of stepped decorative metal roofing panels |
| 4. Finished Product | Glazed-style color steel roof tile sheets |
| 5. Raw Material | Pre-painted steel, galvanized steel, Galvalume, or aluminum coil |
| 6. Material Form | Continuous metal coil |
| 7. Common Thickness Range | Typically around 0.3-0.8 mm, subject to profile and material strength |
| 8. Coil Feeding Width | Customized according to the required panel profile |
| 9. Effective Cover Width | Defined by the approved roof sheet drawing |
| 10. Profile Options | Glazed tile, Roman tile, classic tile, or custom architectural profile |
| 11. Tile Pitch | Configured or programmed according to customer requirements |
| 12. Tile Step Height | Customized through the hydraulic die and profile design |
| 13. Rib Height | Manufactured according to the confirmed section drawing |
| 14. Forming Method | Continuous multi-pass cold roll forming |
| 15. Forming Stations | Selected according to profile complexity and material thickness |
| 16. Roller Material | Precision-machined high-grade steel |
| 17. Roller Surface Treatment | Optional polishing, hardening, or chrome plating |
| 18. Roller Processing | CNC machining for stable dimensions and repeatable profiles |
| 19. Main Shaft Material | Heat-treated high-strength steel |
| 20. Shaft Diameter | Engineered according to forming load and machine model |
| 21. Main Frame | Heavy-duty welded steel base |
| 22. Frame Processing | Stress-relieved and machined for accurate station alignment |
| 23. Side Support Structure | Guide-post, wall-panel, or modular support design |
| 24. Drive System | Electric motor with chain, gearbox, or combined transmission |
| 25. Main Motor Power | Matched to line speed, material thickness, and roof profile |
| 26. Speed Regulation | Variable-frequency drive available for smooth adjustment |
| 27. Production Speed | Project-specific and coordinated with the hydraulic pressing cycle |
| 28. Feeding Guide | Adjustable guide for accurate strip entry |
| 29. Leveling Unit | Optional pre-leveler for improved incoming strip flatness |
| 30. Tile Pressing System | Hydraulic step-forming press |
| 31. Pressing Die | Profile-specific die for repeatable tile shape |
| 32. Cutting System | Hydraulic profile-following cutting unit |
| 33. Cutting Mode | Stop-to-cut or synchronized configuration by project |
| 34. Cutting Blade | Hardened tool steel designed for the specified sheet material |
| 35. Length Measurement | Encoder-based automatic measurement |
| 36. Length Setting | Entered through the touch-screen HMI |
| 37. Quantity Setting | Programmable batch quantity control |
| 38. Control System | Industrial PLC control cabinet |
| 39. Operator Interface | Movable color touch-screen panel |
| 40. Control Modes | Automatic, manual, and jog operation |
| 41. Production Monitoring | Displays panel length, quantity, status, and alarm information |
| 42. Emergency Stop | Dedicated emergency-stop circuit and push button |
| 43. Electrical Components | Industrial-grade components with preferred brands available |
| 44. Hydraulic Station | Independent power unit for pressing and cutting |
| 45. Hydraulic Pressure | Configured according to tile-step depth and cutting load |
| 46. Hydraulic Cooling | Optional cooling system for extended production shifts |
| 47. Lubrication | Manual or centralized lubrication for transmission points |
| 48. Power Supply | Customized voltage, phase, and frequency |
| 49. Machine Finish | Industrial anti-corrosion paint |
| 50. Machine Color | Standard finish or customized RAL color |
| 51. Decoiler Type | Manual, hydraulic, or motorized decoiler |
| 52. Coil Capacity | Selected according to coil weight and production requirements |
| 53. Coil Loading Car | Optional hydraulic coil car for heavy material handling |
| 54. Receiving Table | Simple support table or roller conveyor |
| 55. Automatic Stacker | Optional for higher automation and reduced manual handling |
| 56. Protective Film Device | Optional unit for protecting coated sheet surfaces |
| 57. Punching Function | Optional hydraulic or servo pre-punching system |
| 58. Embossing Function | Optional decorative or reinforcing embossing unit |
| 59. Automation Level | Semi-automatic or fully automatic configuration |
| 60. Surface Protection | Optimized rollers and guides help reduce scratches |
| 61. Noise and Vibration | Rigid frame and aligned transmission support smoother operation |
| 62. Installation Method | Floor-mounted with leveling and anchoring positions |
| 63. Operator Requirement | Normally one trained operator with material-handling assistance |
| 64. Profile Customization | Based on customer drawing, sample, or dimensional data |
| 65. Profile Change Option | Fixed-profile, cassette, or special quick-change design |
| 66. Suitable Industries | Roofing factories, building-material plants, and steel structure companies |
| 67. Building Applications | Villas, houses, resorts, warehouses, factories, and commercial roofs |
| 68. Maintenance Items | Rollers, bearings, chains, hydraulic oil, sensors, and fasteners |
| 69. Technical Documents | Operation manual, electrical diagram, parts list, and foundation guidance |
| 70. Factory Testing | No-load testing and trial production before shipment |
| 71. Quality Inspection | Checks for panel dimensions, tile pitch, cutting quality, and control accuracy |
| 72. Export Packing | Protected main machine with separately packed electrical and loose parts |
| 73. Shipping Method | Containerized transport based on final line dimensions |
| 74. Installation Support | Remote guidance or on-site service subject to agreement |
| 75. Operator Training | Operation and maintenance training available |
| 76. Spare Parts Service | Consumable and replacement parts can be supplied |
| 77. Language Options | HMI language can be customized |
| 78. Safety Options | Protective guards, warning lights, and safety switches available |
| 79. Remote Diagnostics | Optional remote technical support interface |
| 80. Project Basis | Final specification follows the approved drawing and technical agreement |
How the Glazed Tile Forming Process Works
The flat metal strip enters the machine through an adjustable guide and passes through a sequence of forming rollers. Each station gradually bends the sheet until the required roof profile is completed. The hydraulic press then creates the repeating tile steps at programmed positions. An encoder measures the sheet, and the PLC activates the profile cutter when the target length is reached. The finished panel is discharged onto a support table, conveyor, or automatic stacking system.
Finished Roof Panel Benefits
Traditional tile appearance with lower structural weight
Fast installation and reduced on-site handling
Suitable for long roof spans and customized panel lengths
Compatible with a wide selection of coated steel colors and finishes
Good weather resistance when produced from appropriate coated materials
Useful for both new construction and roof renovation
Customization Options
The production line can be configured for different feeding widths, effective cover widths, tile pitches, step heights, rib depths, material strengths, panel lengths, and production capacities. Optional equipment includes a hydraulic decoiler, coil car, pre-leveler, protective-film applicator, pre-punching unit, servo pressing system, flying cutter, automatic conveyor, stacker, safety enclosure, voltage transformer, and remote diagnostics.
Quality Control Before Delivery
Before shipment, the machine can be inspected for frame alignment, roller rotation, transmission performance, hydraulic pressure, step consistency, encoder accuracy, cutting action, electrical control, and finished-panel dimensions. Trial sheets may be produced with the agreed material to verify profile shape and operating sequence.
Information Required for a Technical Proposal
Please provide the target roof tile drawing, raw material type, material yield strength, thickness range, feeding width, effective cover width, tile pitch, panel length range, target output, coil weight, local power supply, and preferred automation level. A physical panel sample can also be used as a design reference when a detailed drawing is unavailable.
Important: All specifications are configurable. Final motor powers, station quantity, speed, dimensions, weight, and component brands are subject to the approved profile drawing and signed technical agreement.
- User name Member Level Quantity Specification Purchase Date
- Satisfaction :
-