- Trapezoidal Machine
- Corrugated Machine
- Glazed Tile Machine
- Double Layer Machine
- CZU Purlin Machine
- Ridge Cap Machine
- Floor Decking Machine
- Rolling Door Machine
- Fence Machine
- Embossing Machine
- Standing Seam Machine
- Cut To Length And Slitting Line
- Guard Rail Machine
- Decoiler And Stacker
- Stud And Track Machine
- Gutter And DownPipe
- Curving Machine
- Cladding Panel Machine
- Corollary Equipment

- Trapezoidal Machine
- Corrugated Machine
- Glazed Tile Machine
- Double Layer Machine
- CZU Purlin Machine
- Ridge Cap Machine
- Floor Decking Machine
- Rolling Shutter Door Machine
- Palisade Fence Machine
- Embossing Machine
- Standing Seam Machine
- Cut To Length And Slitting Line
- Guard Rail Machine
- Decoiler And Stacker
- Stud And Track Machine
- Gutter And DownPipe
- Curving Machine
- Cladding Panel Machine
- Corollary Equipment
- Other
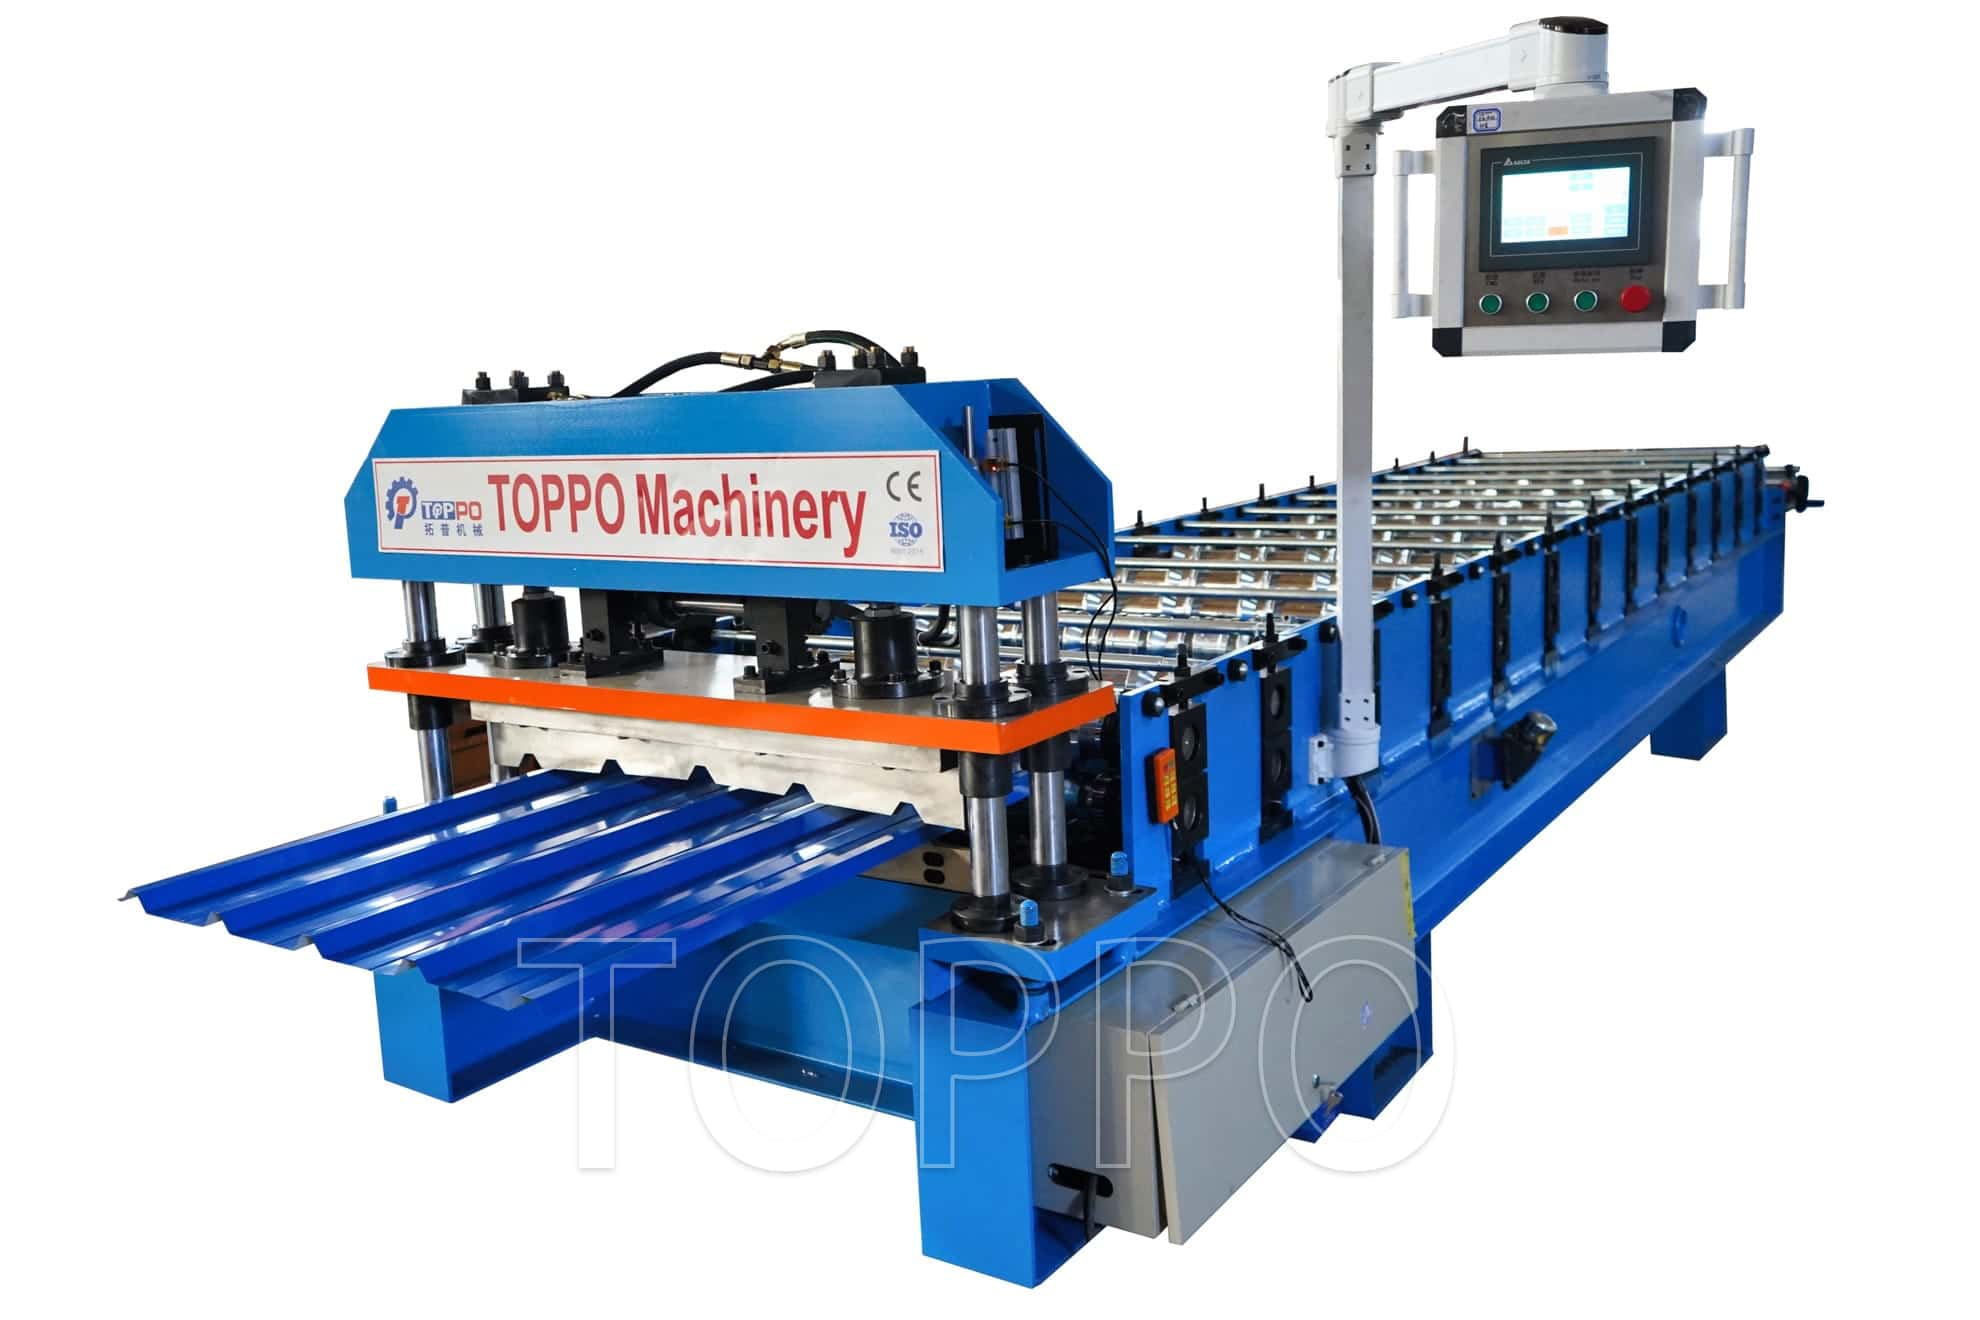
Automatic Trapezoidal Metal Roof Sheet Roll Forming Machine
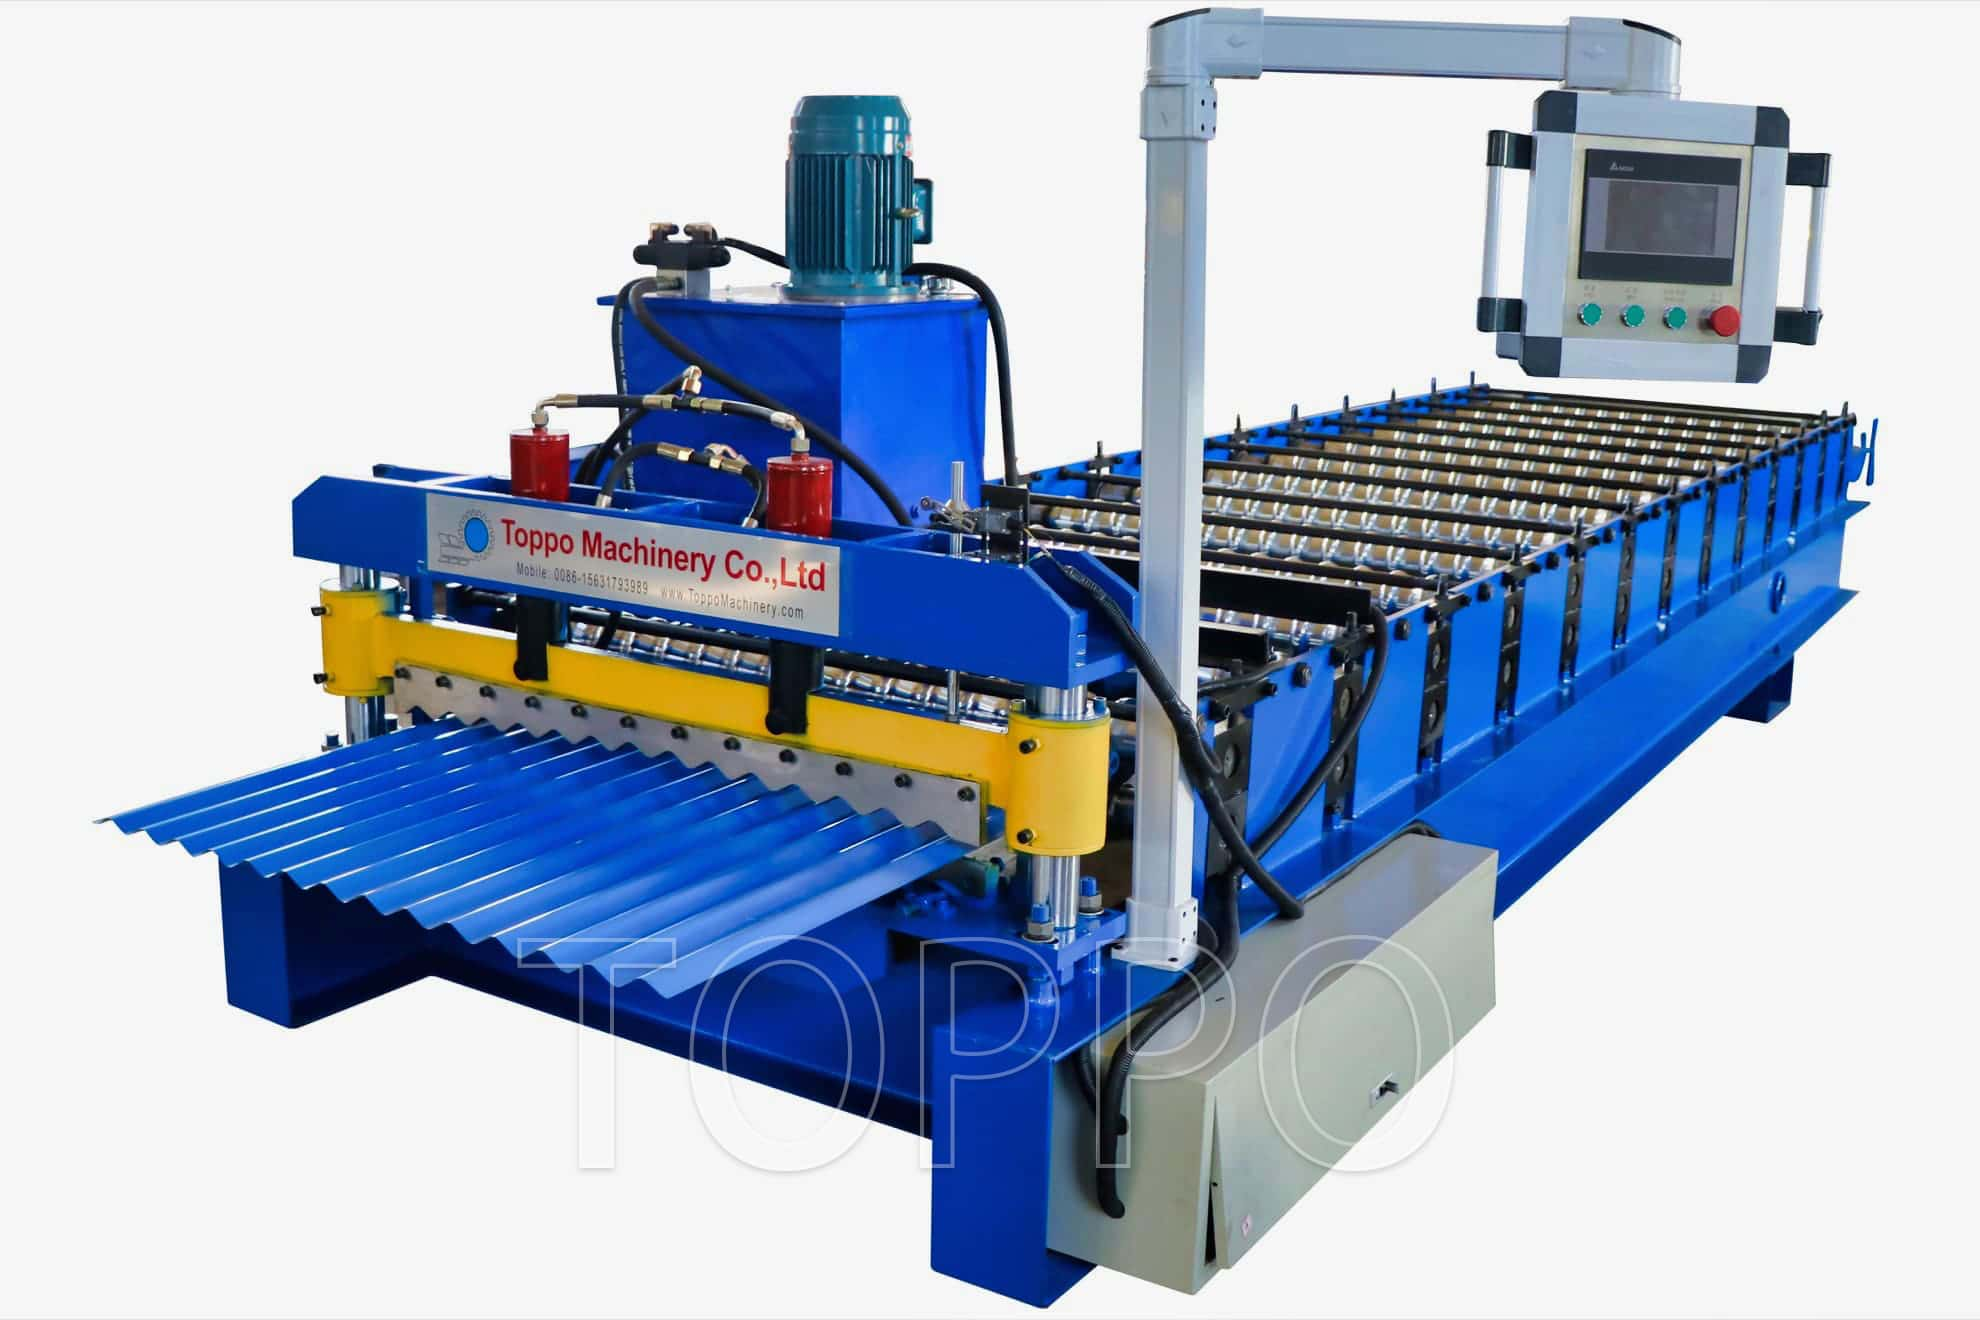
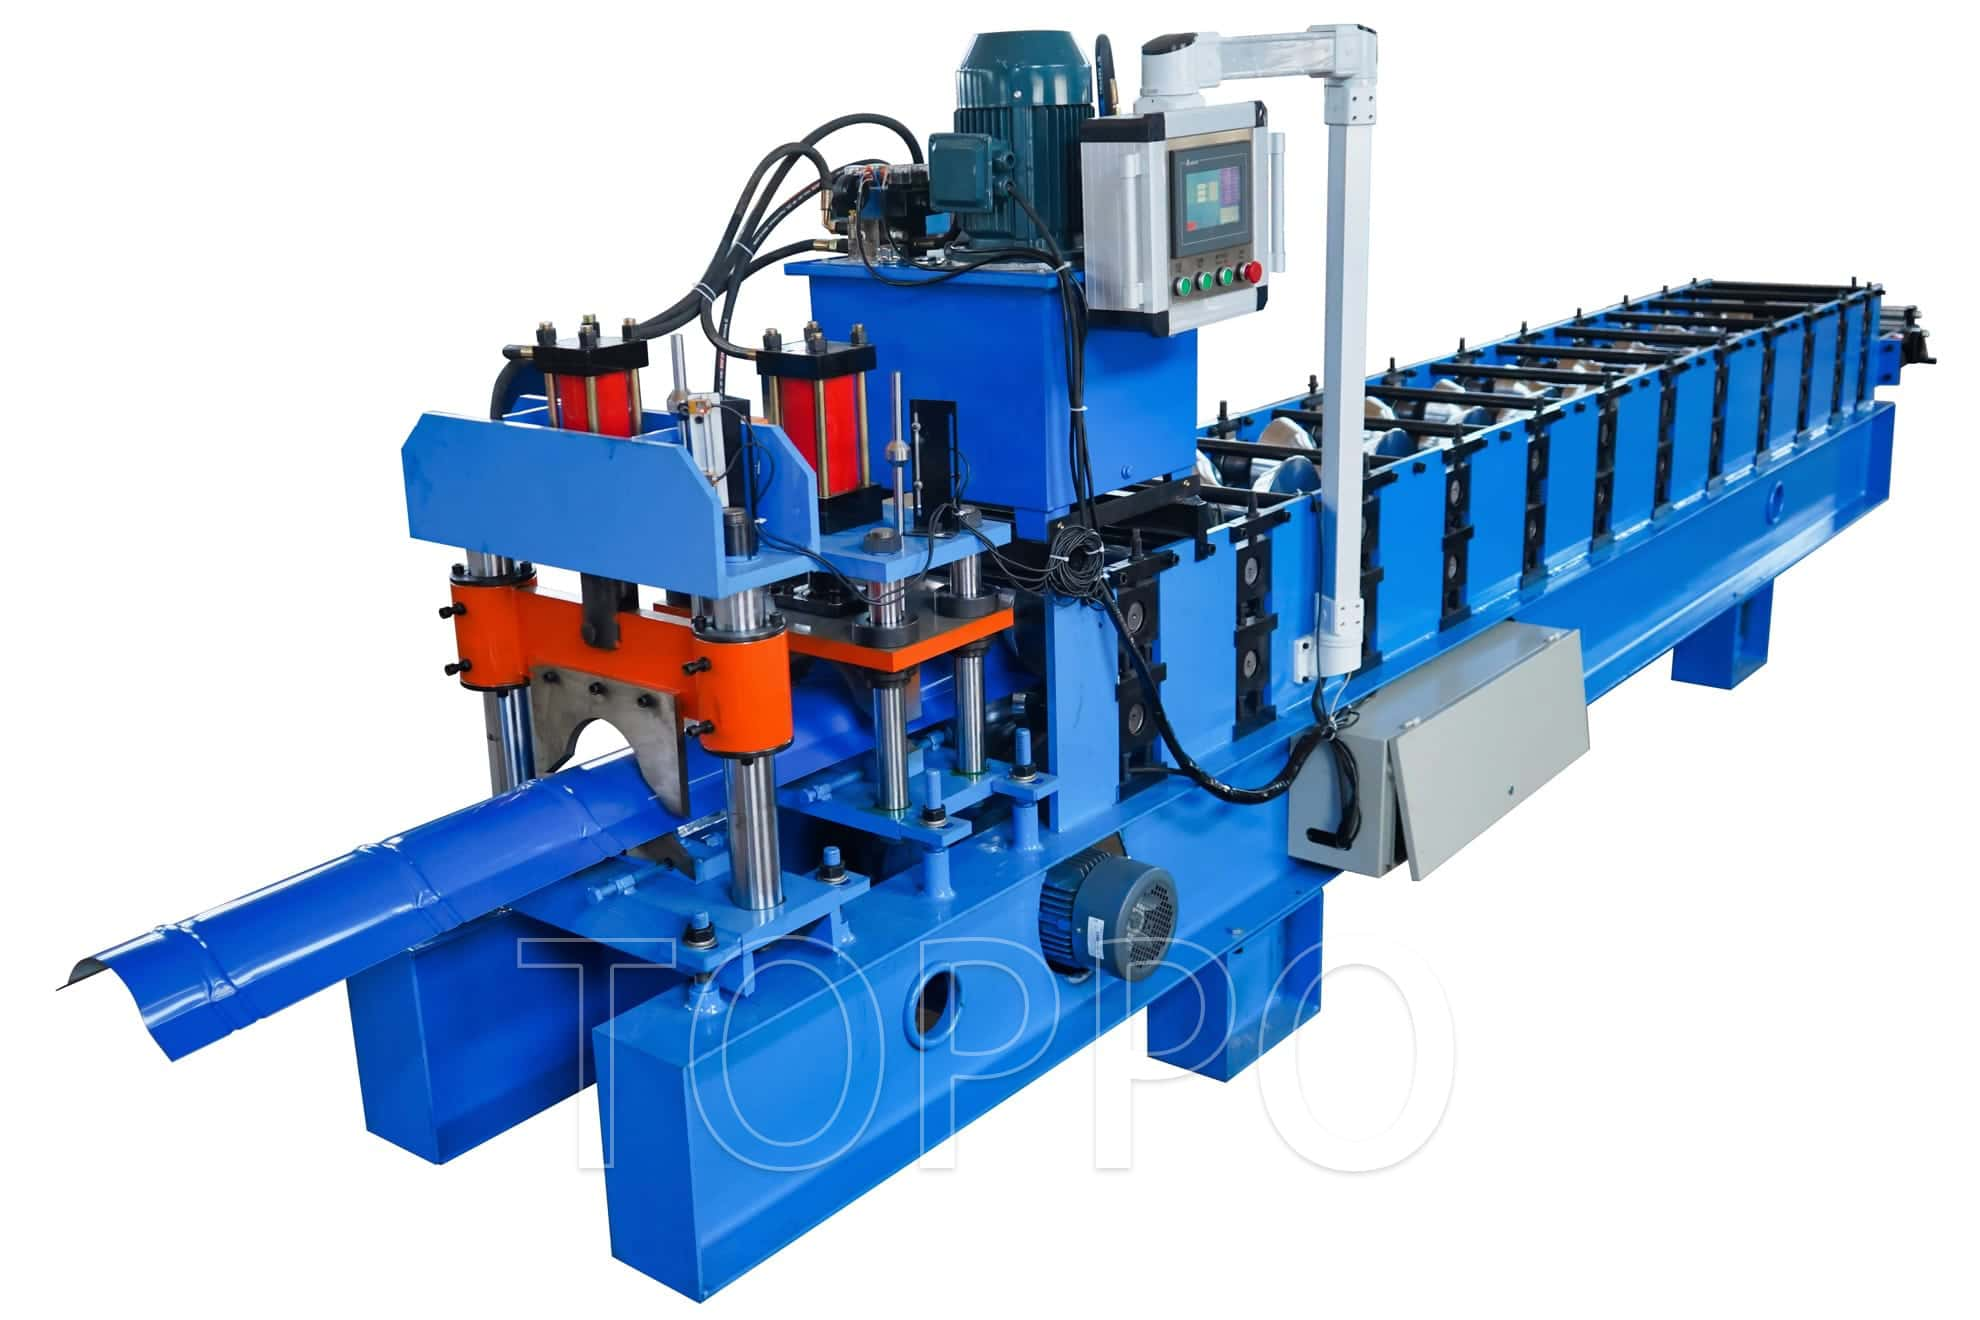
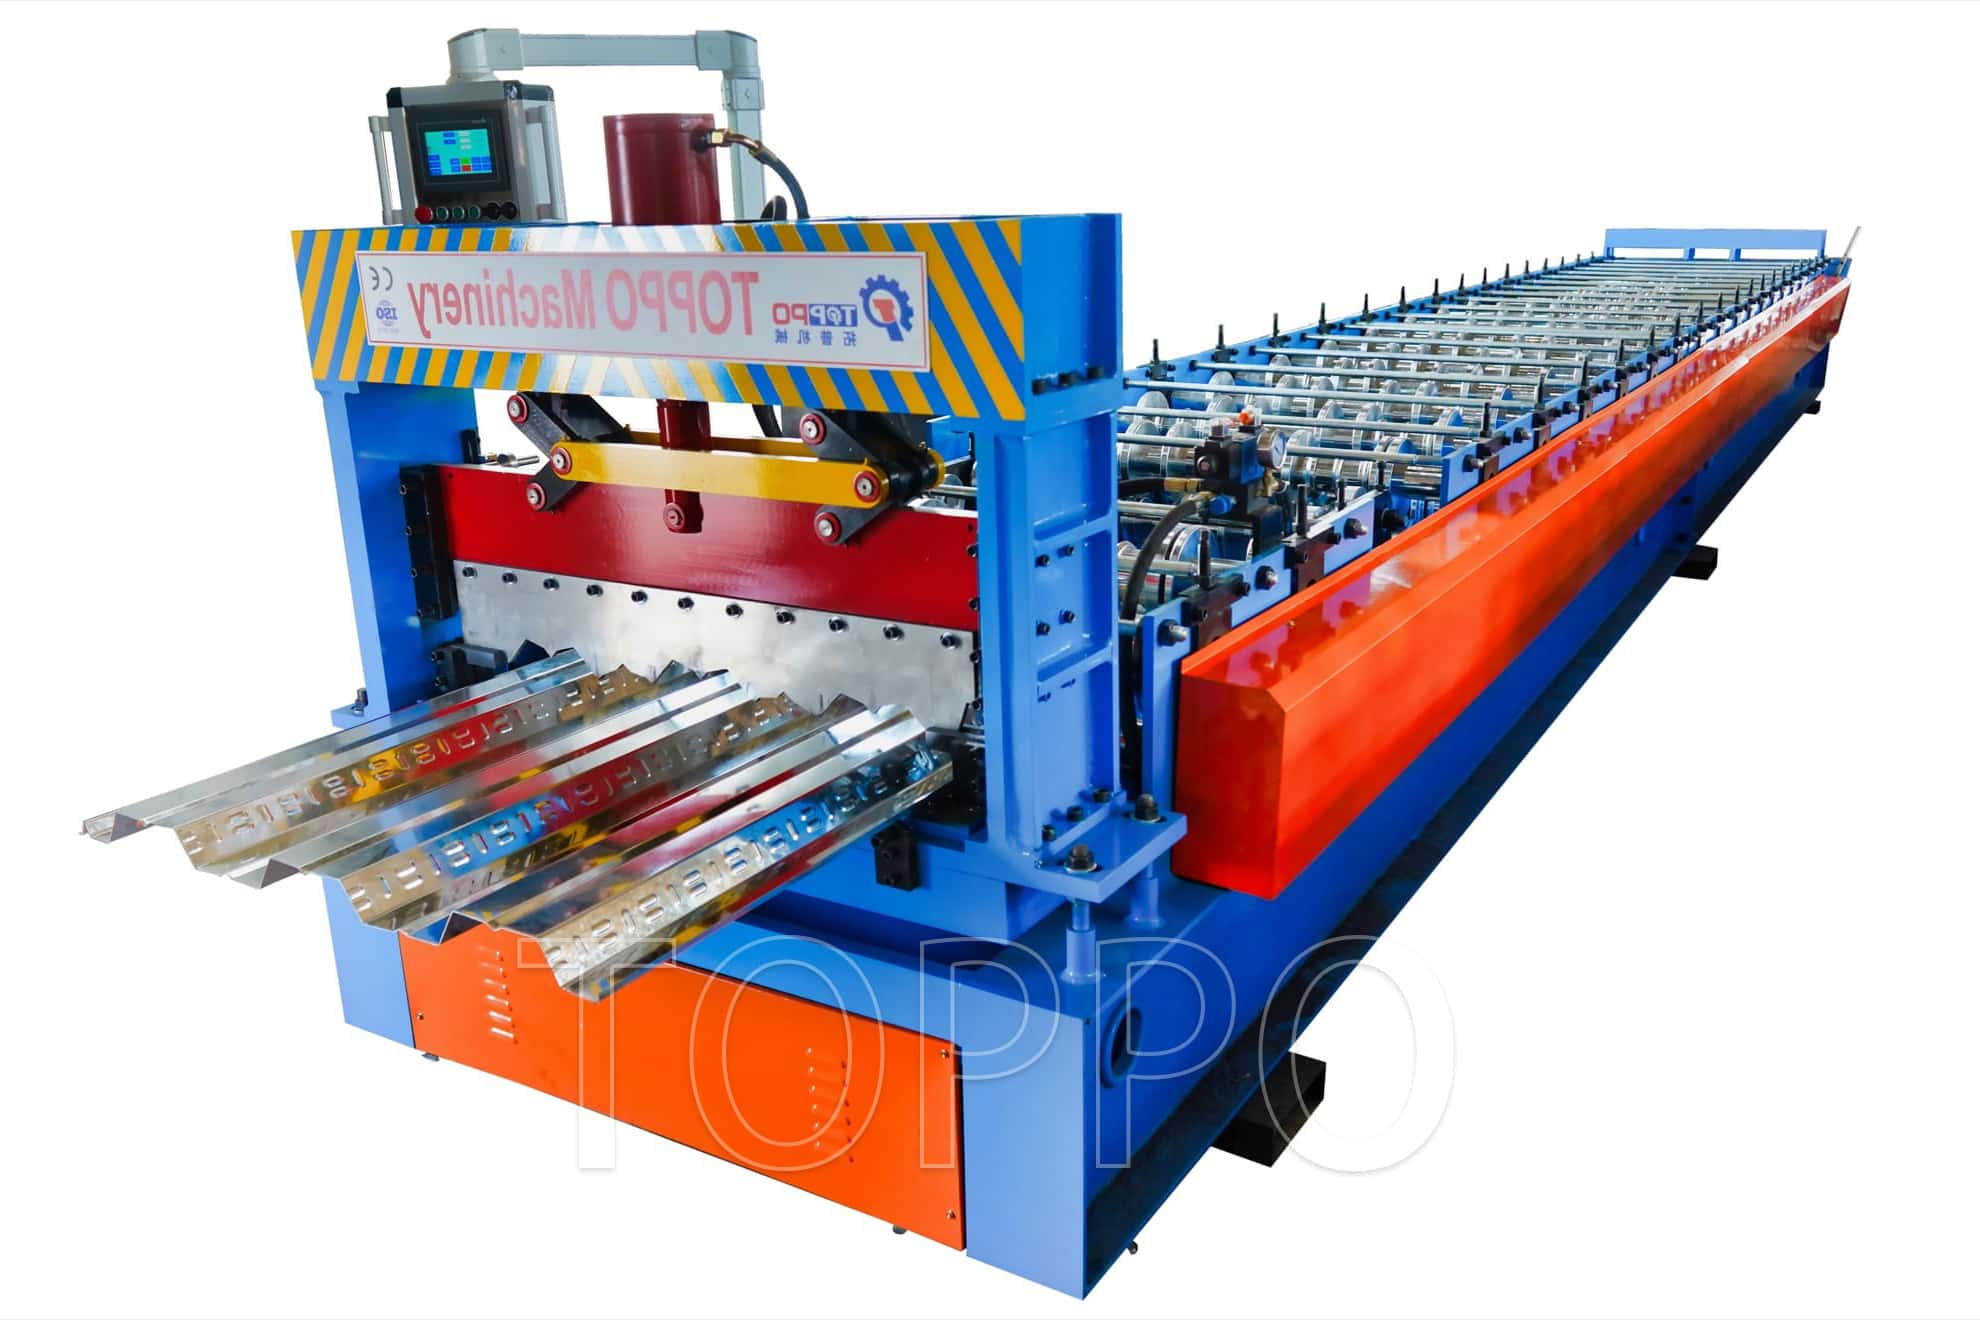
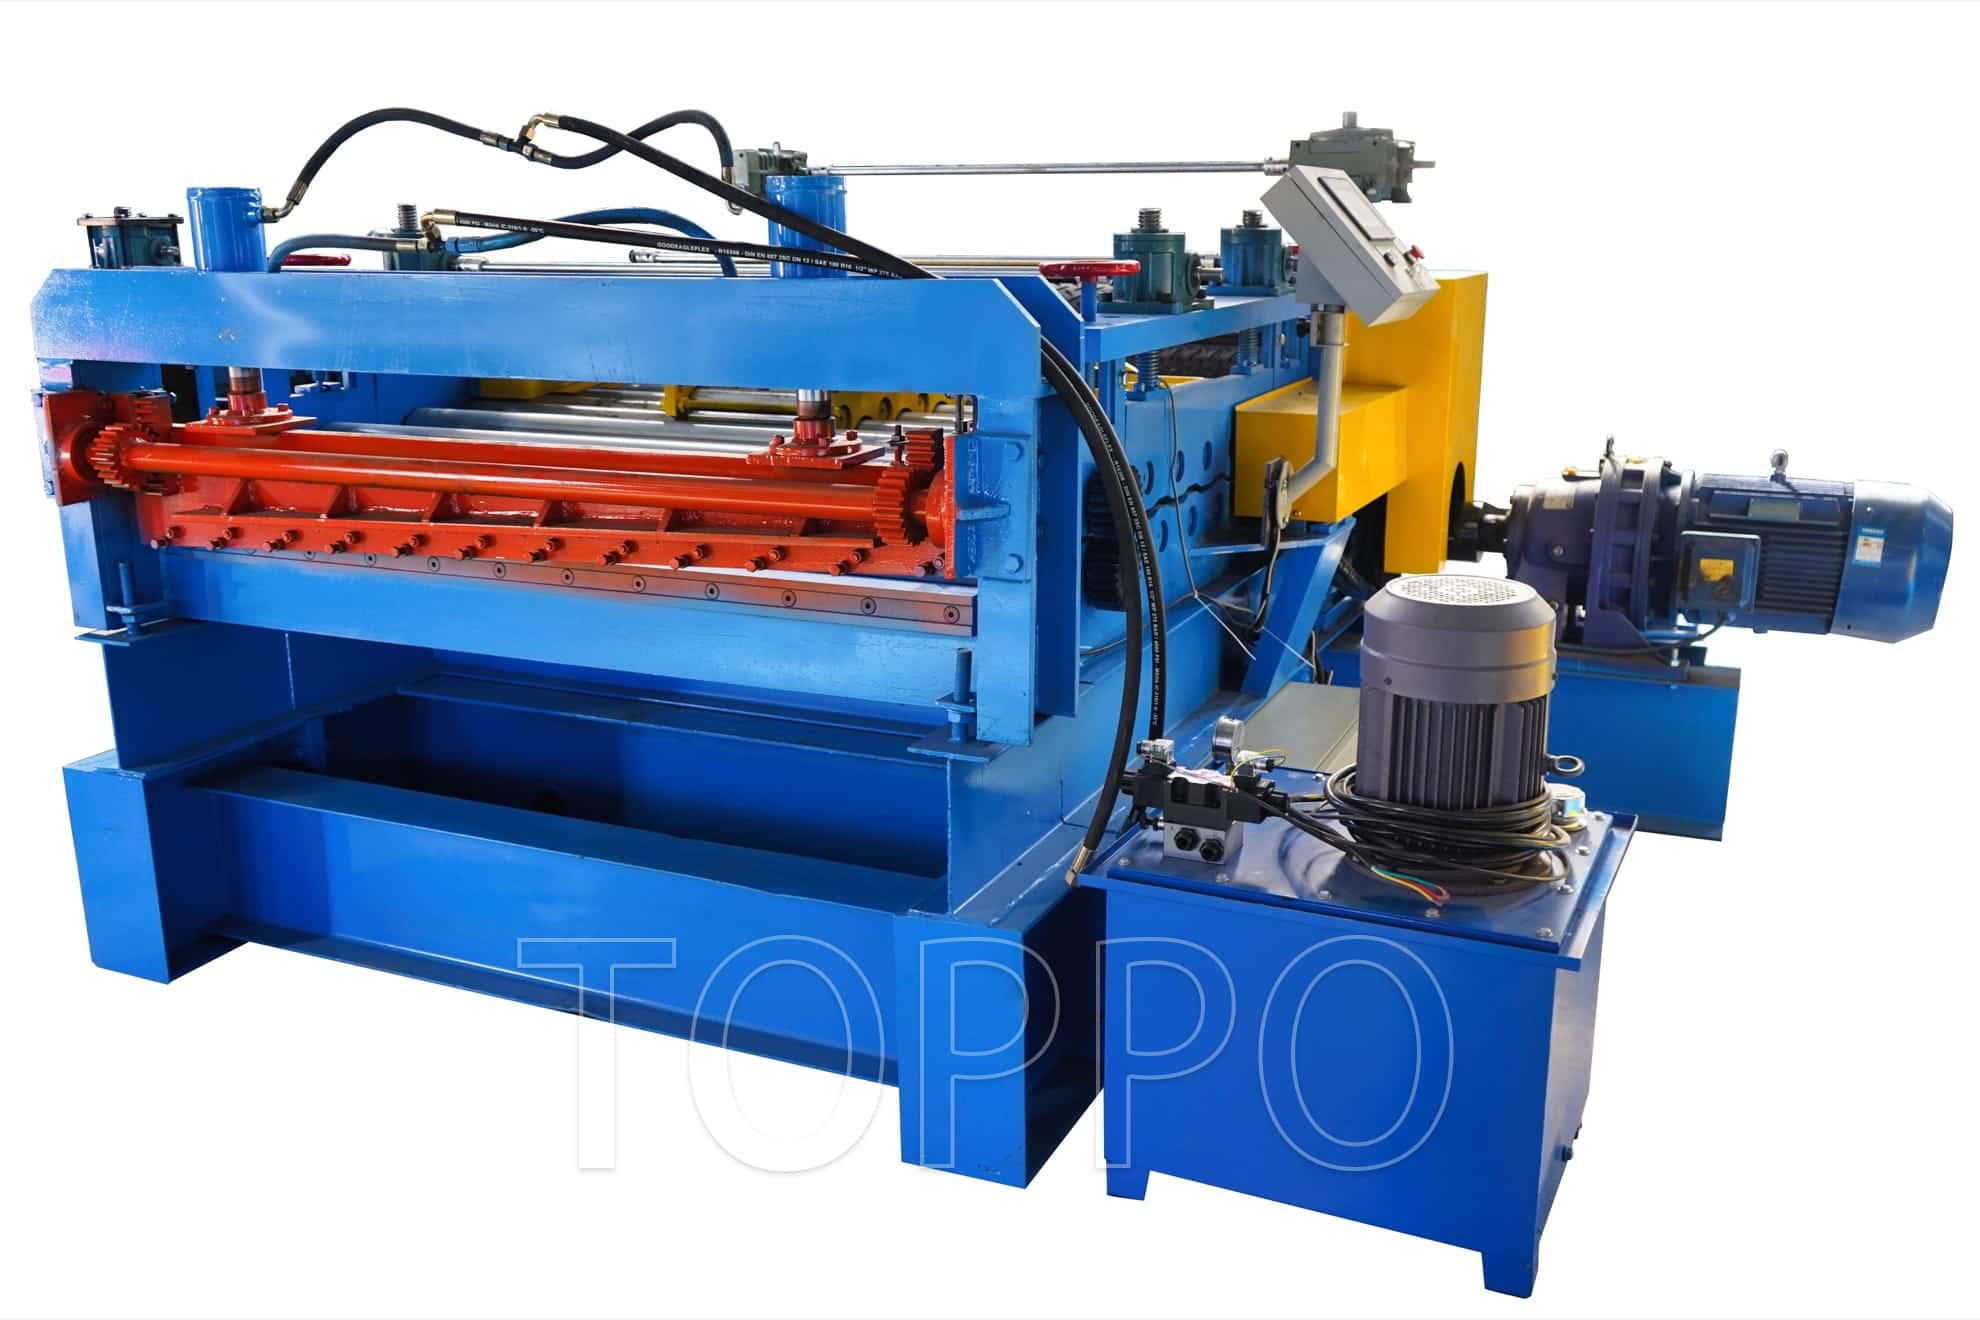
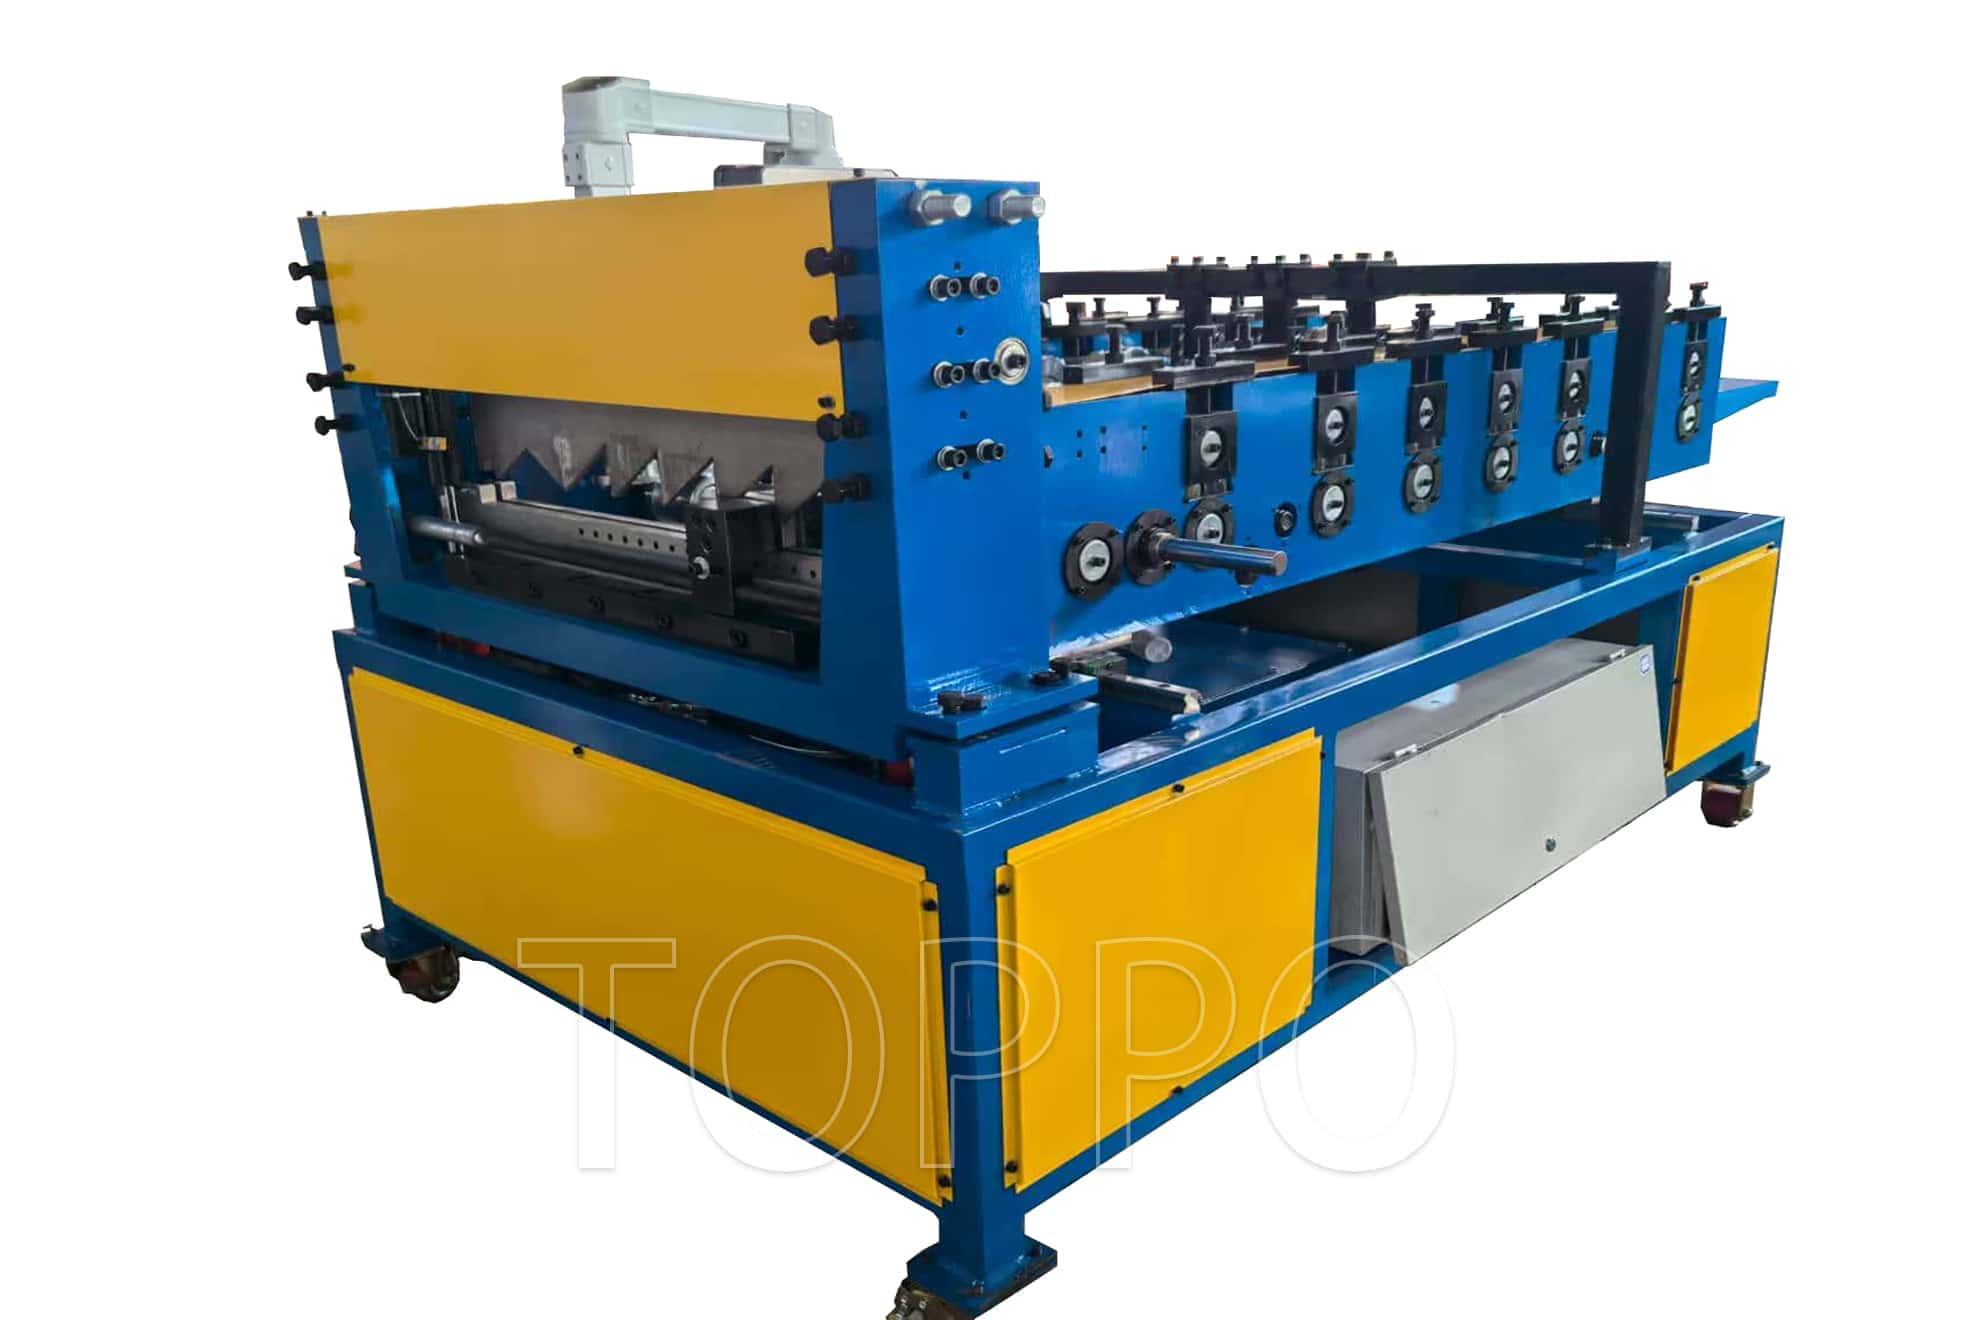
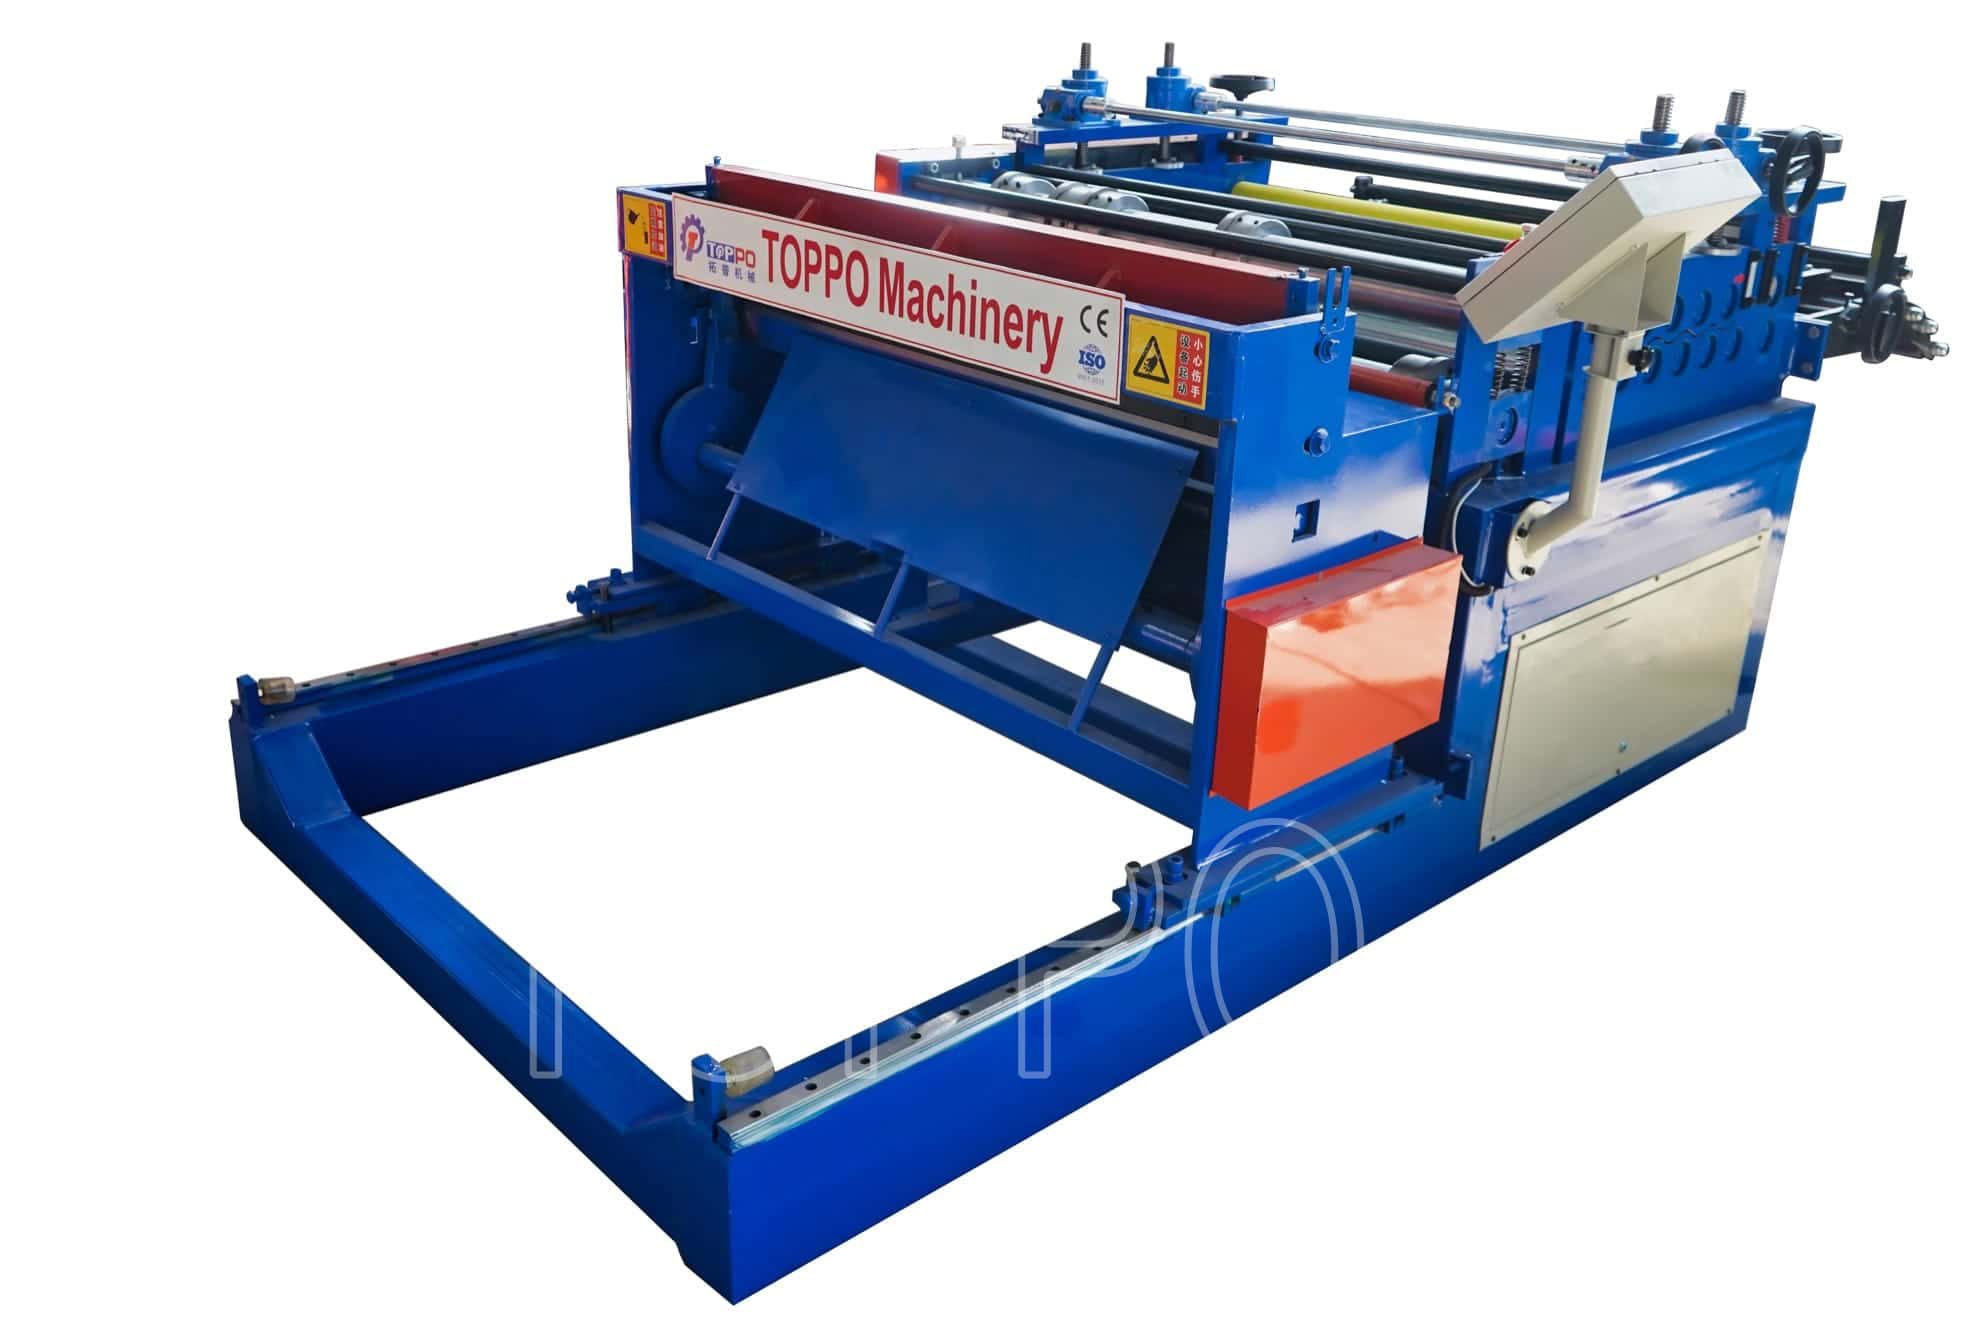
The TOPPO trapezoidal roof panel roll forming machine is an industrial cold-forming line for producing consistent metal roofing and wall cladding sheets with trapezoidal ribs. The machine configuration shown combines a rigid welded base, multiple precision roller stations, an integrated hydraulic cutting assembly and an electrical control cabinet positioned beside the line for convenient operation.
Metal coil enters through the feeding guide, passes progressively through the forming rollers and is shaped into the required roof profile without heating. A rotary encoder measures panel length, the PLC controls production quantity, and the hydraulic cutter separates each finished sheet automatically. The result is a repeatable panel profile suitable for warehouses, workshops, agricultural buildings, garages, commercial facilities and prefabricated structures.
Key Advantages
Automatic coil-to-panel production with PLC control
Stable trapezoidal ribs and repeatable panel geometry
Touch-screen setting of length, quantity and production batches
Hydraulic cutting for accurate and clean panel ends
Heavy-duty welded frame for long-term industrial operation
Precision-machined rollers help protect coated sheet surfaces
Adjustable feeding guides improve strip alignment
Manual, jog and automatic operating modes
Custom roller tooling for different roof and wall panel profiles
Optional decoiler, leveling, punching, film laminating and stacking systems
Typical Technical Attributes
Note: The following parameters are typical reference values. Final specifications are engineered according to the customer's panel drawing, raw material, thickness range, yield strength, required speed and local electrical standard.
| Attribute | Typical / Customizable Specification |
|---|---|
| 1. Product name | Automatic Trapezoidal Metal Roof Sheet Roll Forming Machine |
| 2. Machine category | Automatic cold roll forming production line |
| 3. Finished product | Trapezoidal roofing sheet and wall cladding panel |
| 4. Forming process | Continuous multi-station cold roll forming |
| 5. Profile design | Customized according to customer drawing or sample |
| 6. Suitable materials | PPGI, PPGL, galvanized steel, Galvalume and aluminum coil |
| 7. Typical material thickness | 0.30-0.80 mm, customizable |
| 8. Typical coil width | 914-1250 mm or profile dependent |
| 9. Material yield strength | Typically 230-550 MPa, subject to engineering confirmation |
| 10. Finished panel width | Determined by input width and profile geometry |
| 11. Effective cover width | Customized for the required roofing system |
| 12. Rib shape | Trapezoidal |
| 13. Rib height | Customized according to profile drawing |
| 14. Rib pitch | Customized according to profile drawing |
| 15. Panel length | Programmable through the HMI |
| 16. Typical forming speed | 10-20 m/min, excluding cutting time |
| 17. High-speed option | Available with upgraded drive and flying cut |
| 18. Forming stations | Typically 12-18 stations, profile dependent |
| 19. Roller material | 45# steel or suitable alloy steel |
| 20. Roller machining | CNC precision machining |
| 21. Roller surface treatment | Polishing, hard chrome plating or heat treatment |
| 22. Shaft material | 45# steel or equivalent |
| 23. Typical shaft diameter | Approximately 70-85 mm, selected by load calculation |
| 24. Main frame | Heavy welded steel structure |
| 25. Frame processing | Stress relieved and precision machined where required |
| 26. Side wall structure | Plate-type or stand-type forming structure |
| 27. Main drive | Electric motor with gearbox and chain or gear transmission |
| 28. Typical main motor power | 5.5-11 kW, profile and speed dependent |
| 29. Transmission type | Chain, gear or gearbox drive |
| 30. Feeding guide | Adjustable left-right side guide |
| 31. Entry leveling | Optional leveling or straightening unit |
| 32. Cutting type | Hydraulic post-cut or pre-cut system |
| 33. Cutting blade material | Cr12MoV, D2 or equivalent tool steel |
| 34. Hydraulic station | Independent hydraulic power unit |
| 35. Typical hydraulic power | 4-7.5 kW, configuration dependent |
| 36. Length measurement | Rotary encoder |
| 37. Typical cutting accuracy | Approximately ±1.5 mm under normal operating conditions |
| 38. Control system | PLC automatic control |
| 39. Operator interface | Touch-screen HMI |
| 40. Control language | English; other languages optional |
| 41. Production modes | Automatic, manual and jog operation |
| 42. Quantity control | Preset pieces and batch production |
| 43. Length input | Digital setting through touch screen |
| 44. Electrical cabinet | Integrated or separate cabinet according to layout |
| 45. Electrical brands | International or customer-specified components available |
| 46. Power supply | 380 V, 50 Hz, 3 phase or customized |
| 47. Emergency stop | Accessible emergency stop circuit |
| 48. Safety guarding | Optional protective covers and interlocks |
| 49. Decoiler type | Manual, hydraulic or automatic decoiler |
| 50. Typical decoiler capacity | 3-10 tons, customizable |
| 51. Coil inner diameter | Commonly 450-610 mm, adjustable |
| 52. Coil outer diameter | Configured according to coil weight and workshop layout |
| 53. Run-out support | Manual support table or automatic stacker |
| 54. Automatic stacking | Optional |
| 55. Online punching | Optional hydraulic or servo punching |
| 56. Film laminating | Optional protective film device |
| 57. Lubrication | Manual or centralized lubrication system |
| 58. Machine color | Factory standard or customer RAL color |
| 59. Machine dimensions | Determined by profile, station quantity and accessories |
| 60. Machine weight | Determined by final heavy-duty configuration |
| 61. Installation layout | Customized layout drawing supplied before production |
| 62. Operating environment | Indoor industrial workshop |
| 63. Surface protection | Roller finish designed to minimize scratches on coated sheet |
| 64. Main applications | Roofing, wall cladding, warehouses, workshops and agricultural buildings |
| 65. Documentation | Operation manual, electrical drawing and installation layout |
| 66. Training | Operation and maintenance training available |
| 67. Installation support | Online guidance or on-site service by agreement |
| 68. Warranty | Manufacturer warranty according to sales contract |
| 69. Spare parts | Recommended spare-parts package available |
| 70. Customization | Profile, speed, voltage, brands, color and automation options |
Working Process
Coil loading → decoiling → feeding and alignment → optional leveling → progressive roll forming → encoder length measurement → hydraulic cutting → panel discharge → optional automatic stacking.
Applications
The finished trapezoidal sheets are widely used for industrial plants, logistics warehouses, steel structure workshops, agricultural sheds, garages, commercial buildings, modular houses, temporary structures, wall cladding systems and general metal roofing projects. Different rib heights, pitches and cover widths can be produced by designing dedicated roller tooling and cutting dies.
Customization Options
Single-layer, double-layer or cassette-type forming line
Manual, hydraulic or automatic decoiler
Pre-cutting, post-cutting or servo flying cutting
Entry leveling and coil guiding system
Protective film laminating device
Online hole punching or embossing unit
Automatic stacking and discharge conveyor
Customized PLC, inverter and electrical component brands
Remote diagnostics and production data interface
Customized voltage, frequency, language and machine color
Production and Quality Control
Before delivery, the frame, rollers, shafts, transmission, hydraulic system, cutting die and PLC program are assembled and tested as a complete line. Trial production is carried out with suitable coil material to verify profile dimensions, surface condition, panel straightness, cutting accuracy and automatic operation. Inspection records and operating documents can be supplied with the machine.
Operation and Maintenance
Operators should keep the feeding centerline aligned, inspect chains and fasteners regularly, maintain the hydraulic oil at the correct level and lubricate moving parts according to the maintenance schedule. Forming rollers should be kept clean to avoid marks on coated steel. Electrical and hydraulic work should only be carried out by qualified personnel with the machine isolated from power.
Packing and Delivery
Main machine components are secured for container shipment. Exposed metal surfaces receive anti-rust protection, electrical cabinets are moisture protected, and loose accessories are packed separately. A loading plan, foundation information and installation layout can be prepared before dispatch.
Frequently Asked Questions
Can one machine produce several profiles?
A conventional roller set normally produces one specified profile. A double-layer or cassette-type machine can be designed when multiple profiles are required.
What information is required for a quotation?
Please provide the profile drawing, raw material, thickness range, coil width, yield strength, desired speed, power supply and preferred auxiliary equipment.
Can the machine process high-strength steel?
Yes. Shaft diameter, roller stations, drive power and frame structure are engineered according to material strength and profile geometry.
Is the line tested before shipment?
Yes. The production line is assembled, programmed and trial-run before dispatch, subject to the agreed material and acceptance procedure.
- User name Member Level Quantity Specification Purchase Date
- Satisfaction :
-